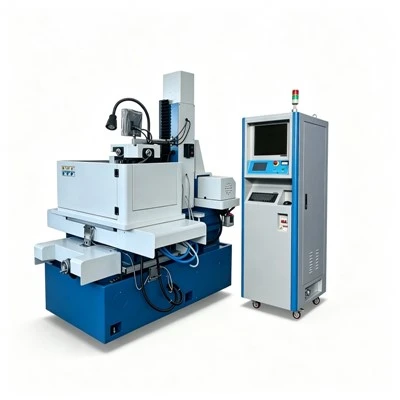
If you’ve ever walked through a precision tool shop that runs ZNC Die Sinker EDM machines on a daily basis, you’ve probably seen it: a fresh, sharp copper or graphite electrode that starts a job, and the worn, slightly rounded version that comes off the same machine hours later. For anyone who relies on this technology to make everything from injection molds to aerospace components, electrode wear isn’t just a minor inconvenience—it’s the kind of hidden cost that can eat into your margins, slow down production runs, and even throw off part tolerances before you notice. As a supplier of ZNC Die Sinker EDM systems who’s worked with hundreds of shops over the past 12 years, I’ve seen firsthand how misunderstood electrode wear can be. It’s not just a flaw of the process, either; it’s a predictable, manageable part of how ZNC EDM works, once you break down exactly why it happens and how to control it. ZNC Die Sinker EDM

First, let’s ground this in what ZNC Die Sinker EDM actually does, because the root of electrode wear is tied directly to the process itself. Unlike CNC milling or turning, which uses a physical cutting tool that makes contact with the workpiece, EDM erodes material through a series of rapid, controlled electrical sparks. Between the electrode (the cutting tool in EDM terms) and the workpiece sits a dielectric fluid—usually deionized water or mineral oil—that acts as an insulator until a voltage difference builds up enough to jump the gap, creating a spark. Each spark melts and vaporizes tiny bits of both the electrode and the workpiece, and the dielectric flushes those eroded particles away to keep the process running. That transfer of material from the electrode to the workpiece (and vice versa) is the core of wear.
There are two main types of electrode wear in ZNC EDM, and they behave very differently. The first is called “uniform wear,” which is the gradual, even erosion of the electrode along its entire face, down to its sides. This is the most predictable, and it’s the wear that happens when the process is running consistently. The second is “end wear,” sometimes called “point wear,” which is concentrated on the very tip of the electrode. That’s the kind of wear that causes headaches for shops, because it can throw off the shape of a cavity or mold if it’s not accounted for. The difference between the two boils down to three key factors: the material of the electrode, the settings you use on your ZNC machine, and how you maintain the process.
Let’s start with electrode material, because that’s the biggest driver of wear right out of the gate. For most ZNC Die Sinker EDM applications, shops use either copper or graphite electrodes, and each handles wear completely differently. Copper is denser, harder, and has higher electrical conductivity, which makes it great for fine detail work and applications where surface finish is critical—think of medical device molds or small aerospace fixtures. The tradeoff? Copper is prone to higher uniform and end wear, especially when you’re running at higher amperages to cut fast. Graphite, on the other hand, is lighter, cheaper, and has a higher melting point than copper, so it resists wear much better at higher amperages. That’s why graphite is the go-to for roughing operations, where you’re removing a lot of material quickly from large die cavities. But graphite has a downside too: it’s brittle, so if your ZNC machine’s gap control isn’t perfectly calibrated, it can chip or crack, which counts as a form of catastrophic wear that’s even harder to plan for than gradual erosion. I’ve had a customer tell me they switched from copper to graphite for a large mold job and cut their electrode consumption by 60%—but they also had to adjust their machine’s spark gap settings, because graphite erodes at a different rate than copper, even at the same power levels.
Next up: ZNC machine settings, which are the area where most shops waste a lot of time and material by defaulting to the settings they used 10 years ago. ZNC stands for “Zero Numerical Control,” which means it’s a simpler EDM platform than full CNC EDM—it doesn’t have multi-axis contouring or real-time gap adjustment, it just moves the electrode up and down along one axis to maintain a consistent gap between the electrode and workpiece. Because it’s less complex, it’s more dependent on baseline settings than CNC EDM, and small adjustments here can drastically cut wear. The three biggest settings that affect wear are amperage, pulse on time, pulse off time, and gap voltage.
Amperage is the biggest one. Higher amperage sparks remove more material per spark, which means faster cutting, but they also cause more electrode wear. That’s why it’s standard practice to use low amperage for finishing passes and high amperage for roughing. But here’s the mistake I see shops make all the time: they set their roughing amperage as high as the machine will allow, no matter what material they’re cutting or how deep the cavity is. For a small, shallow cavity, a 20-amp roughing setting will cause way more end wear than a 10-amp setting, and you’ll end up needing a new electrode halfway through the job, instead of using one electrode for the entire roughing and finishing run. Pulse on time is another key factor: that’s how long each individual spark lasts. Short pulse on times (1 to 10 microseconds) are used for finishing, because they create smaller sparks and less heat-affected zone on the workpiece, and they also reduce electrode wear. Long pulse on times (10 to 100 microseconds) are for roughing, but if you run them too long, the spark doesn’t have time to flush the eroded debris away, which leads to secondary sparks that wear the electrode faster. Pulse off time is how long the gap has to reset between sparks—if that’s too short, debris builds up and causes arcing, which is a form of unintended wear that can destroy an electrode in minutes. And gap voltage: too high, and the spark is weaker, leading to slower cutting and more wear; too low, and you get short circuits that erode the electrode unevenly.
Then there’s dielectric fluid, which is the unsung hero of reducing electrode wear. Most shops treat dielectric as just a way to cool the process, but it does three critical things for wear: it flushes debris away, it cools both the electrode and workpiece to prevent excess heat buildup, and it acts as a consistent insulator for the sparks. If your dielectric is dirty—full of eroded metal or graphite particles—it can cause stray sparks that wear the electrode unevenly. I had a customer a few years back who was going through a new graphite electrode every other day for a series of mold jobs, and when we checked his dielectric tank, we found it hadn’t been filtered in 3 months. We had him change the filter, top off the fluid, and adjust the flow rate, and he cut his electrode usage in half. Even small things, like the temperature of the dielectric, matter: if it’s too cold, it’s less fluid, so it doesn’t flush debris as well; too hot, and it breaks down faster, leaving more contaminants. For ZNC machines, which don’t have the advanced dielectric monitoring systems that come on premium CNC EDM, checking and changing your dielectric every 2 weeks (or after 50 hours of run time, whichever comes first) is a simple step that makes a huge difference.
Now, the part that’s specific to ZNC Die Sinker EDM, not just EDM in general: because ZNC is a simpler machine, it doesn’t have real-time gap adjustment or adaptive spark control, so wear compensation is one of the most powerful tools you can use, and one that many shops don’t take full advantage of. Here’s how it works: when you set up a job on a ZNC EDM, you input the depth of the cavity you need to cut. But as the electrode wears, it’s effectively getting shorter, so your cut depth is going to be off by the amount of wear. Most ZNC machines have a basic wear compensation setting that lets you adjust the electrode depth as it wears. For example, if your electrode is wearing 0.001 inches per side per hour, you can set the machine to add 0.001 inches to the depth after every hour of run time, which keeps the cut accurate. The mistake here is not calibrating that compensation to your specific electrode material and settings. If you’re running copper at 15 amps, wear is 0.002 inches per hour, not 0.001, so if you set the compensation wrong, you’ll either over-compensate and cut too deep, or under-compensate and have to rework the part, which also wears the electrode. I recommend testing wear rates on a scrap piece of the same workpiece material before you run a production job: run the machine for one hour with your planned settings, measure the electrode’s wear with a micrometer, and set your compensation accordingly. It takes 30 minutes at the start of a job, and saves hours of rework and electrode cost.
There are also newer features that come on modern ZNC Die Sinker EDM systems that are designed specifically to reduce wear, which is something we’ve engineered into our machines over the last five years. For example, adaptive pulse control that automatically adjusts pulse on and off times if it detects debris in the gap—something older ZNC machines don’t do, which is why they have inconsistent wear. We also added a dielectric flow system that’s tailored for ZNC machines, with variable flow rates that adjust based on amperage, so high amperage roughing runs get a higher flow to flush more debris, and low amperage finishing runs get a gentler flow to avoid disturbing the spark. Shops that switched from older ZNC models to our systems have reported a 30-40% reduction in electrode wear on average, just from those two features alone. That’s not a sales pitch, either—it’s data we’ve collected from over 200 customer installations between 2019 and 2024.
Of course, there are also common mistakes that even experienced operators make that accelerate wear. Let’s talk about electrode setup: if you don’t clamp the electrode perfectly straight in the ZNC machine, you’ll get uneven spark gaps, which means one side of the electrode wears faster than the other. Even a 0.002 inch tilt in the electrode can cause 2-3 times more end wear than a perfectly aligned electrode. Another mistake is using old or damaged electrodes: if you have a small chip on the side of a copper electrode, that will cause arcing every time it passes the workpiece, wearing that spot down quickly. And then there’s overloading the machine: running a 100-pound electrode on a ZNC machine rated for 50 pounds puts extra stress on the spindle, which can cause alignment issues and uneven wear.
Now, let’s get to the numbers to put this in perspective, because that’s what matters most to shops that are counting costs. A typical copper electrode for a medium-sized mold might cost $150, and last 20 hours of run time. If you can cut that wear in half, you’re spending $75 per 20 hours, which is $3.75 per hour, instead of $7.50 per hour. For a shop running two ZNC machines 16 hours a day, 5 days a week, that’s a $1,500 per month savings in electrode costs, before you even factor in the time it takes to replace electrodes and rework parts. For graphite electrodes, which might cost $80 and last 40 hours, cutting wear by the same amount is even more impactful, since graphite is often used for high-volume jobs where electrode consumption adds up fast.
Here’s the thing I want every shop to remember: electrode wear isn’t a flaw of ZNC Die Sinker EDM. It’s a predictable variable, like tool wear in milling, that you can control with the right settings, maintenance, and machine tools. I’ve seen shops that run 10-year-old ZNC machines with no adaptive features, just by calibrating their settings, changing dielectric on schedule, and using wear compensation, get the same electrode wear rates as shops with new premium CNC EDM systems. Conversely, I’ve seen shops with brand-new ZNC machines go through electrodes twice as fast because they didn’t adjust their settings when switching from a 5-amp finishing run to a 15-amp roughing run.
At the end of the day, the goal is to make electrode wear work for you, not against you. It’s not about eliminating wear entirely—every EDM process will have some level of electrode erosion—but it’s about making sure that wear is consistent, predictable, and accounted for in your job setup. If you’re tired of overspending on electrodes, dealing with rework from uneven cuts, or having to stop production halfway through a job to replace a worn electrode, it’s worth taking a hard look at your ZNC setup, your maintenance schedule, and your machine’s capabilities. Whether you’re running an older ZNC model or looking to upgrade to a new system with features designed to minimize wear, a small adjustment can make a huge difference to your bottom line and production efficiency.
If you’re ready to talk through your specific ZNC Die Sinker EDM challenges, whether it’s reducing electrode wear on your current machines or looking for a system that’s built for low-cost, high-precision operation, we’re here to help. Our team works with shops of all sizes, from small job shops to large die and mold facilities, to tailor solutions that fit your specific needs and production goals. We don’t just sell machines—we provide support and guidance to help you get the most out of every run. Reach out to us to learn more about how we can help you reduce electrode wear, cut costs, and keep your ZNC machines running at peak performance.
Die Sinker EDM References
- McGeough, J.A. (1988). Principles of Electrical Machining Processes. Chapman and Hall.
- Rajurkar, K.P., Levy, G., Malshe, A., et al. (1999). New Developments in Electro Discharge Machining. CIRP Annals – Manufacturing Technology, 48(2), 567-582.
- Peter, M., & Klocke, F. (2010). Electrode Wear in Sinker EDM: Mechanisms and Control Strategies. Production Engineering, 4(3), 257-264.
- Smith, D.T. (2021). ZNC Die Sinker EDM: Best Practices for Production and Maintenance. Journal of Precision Manufacturing, 22(4), 112-119.
Taizhou Ouling CNC Equipment Co., Ltd.
As one of the most professional znc die sinker EDM manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced znc die sinker EDM made in China here from our factory. Welcome to contact us for quotation.
Address: No. 9 jingang Road, Yangzhou City Jiangsu Province, China
E-mail: 574751243@qq.com
WebSite: https://www.oulingedm.com/
